9419025933/ 9419018579/ 9419018143


Major Facilities

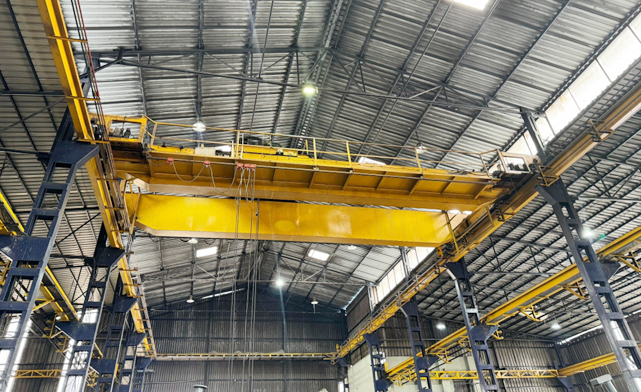
  • 80 Ton Eot Crane
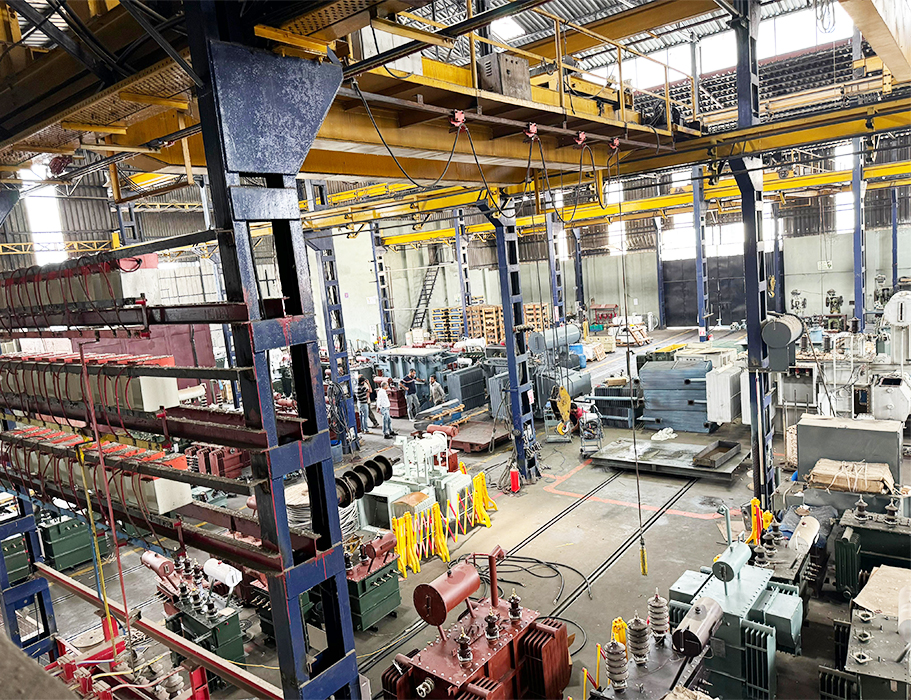
  • AC Dust Proof Winding shop upto 50MVA 132Kv Class
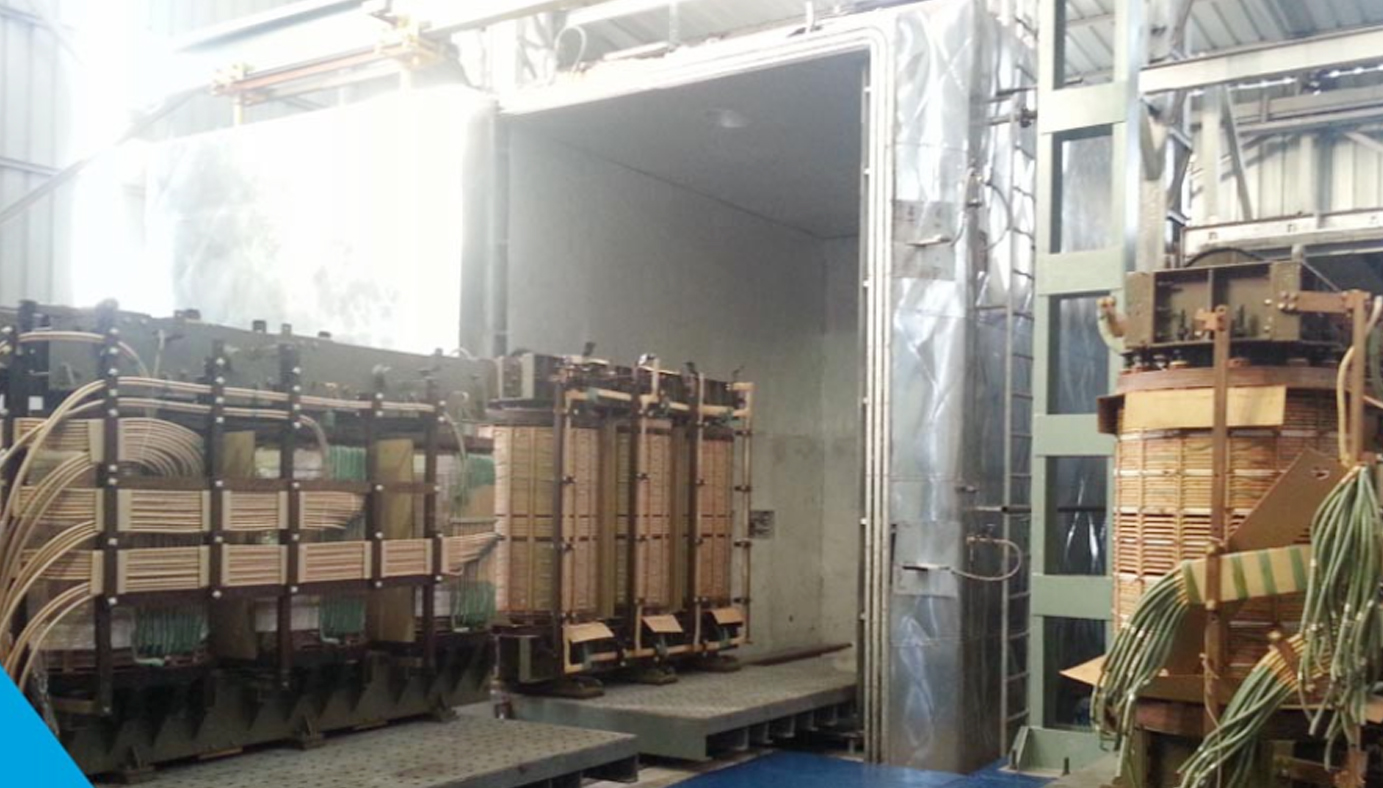
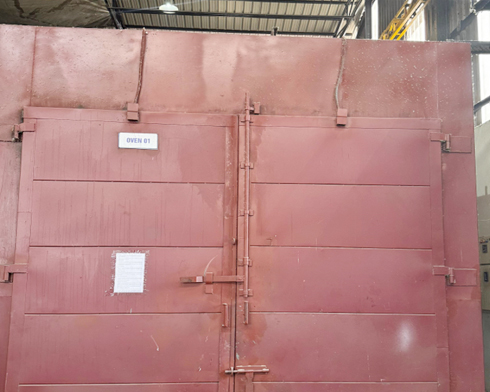
  • Dehydration Oven upto 50MVA 132kV Class
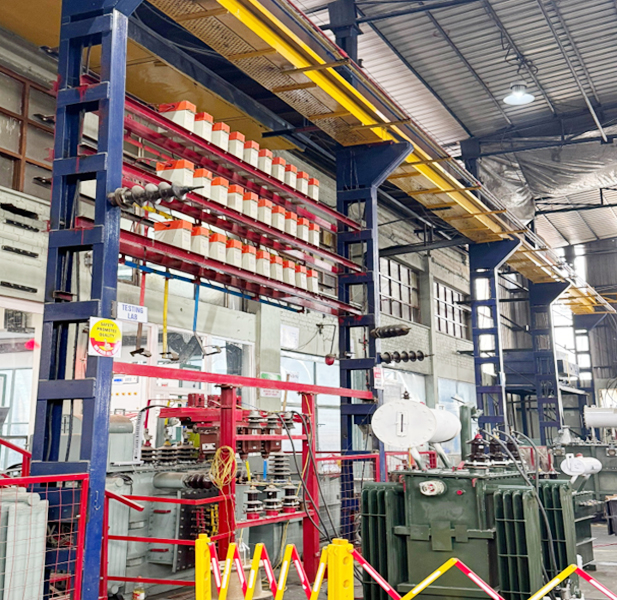
  • In House Testing Facility upto 50MVA 132kV Class
  • In House Heat Run Test Facility upto 50MVA 132kV Class

DEHYDRATION

We have Dehydration Facility upto 50 MVA 220 kV Class.

Another main component besides the core and the winding is the tank of a Power Transformer. It accommodates the active part and the oil filling. After vacuum drying process the active part is removed from the Oven and all components subject to the shrinkage are tightened again. The core & coil assembly is then placed into the tank and property lacked up during the transf read more
BUSINESS ACTIVITY

  • Manufacturing of all types of transformers up to 10MVA 33 kV Class.
  • Manufacturing of 33KV Current and Potential Transformer
  • Manufacturing of Servo Voltage Stabilizer from 10kVA to 2500kVA
  • Manufacuing of LT/HT Panels
  • Manufacturing of Steel Tubular Poles
  • Manufacturing of PVC Wire Conduit Pipes and its Fittings
  • Repairing Up to 50 MVA 132 kV Class

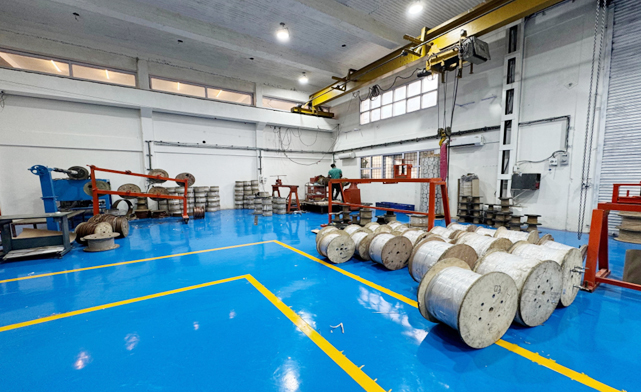
DUST PROOF AC WINDING SHOP

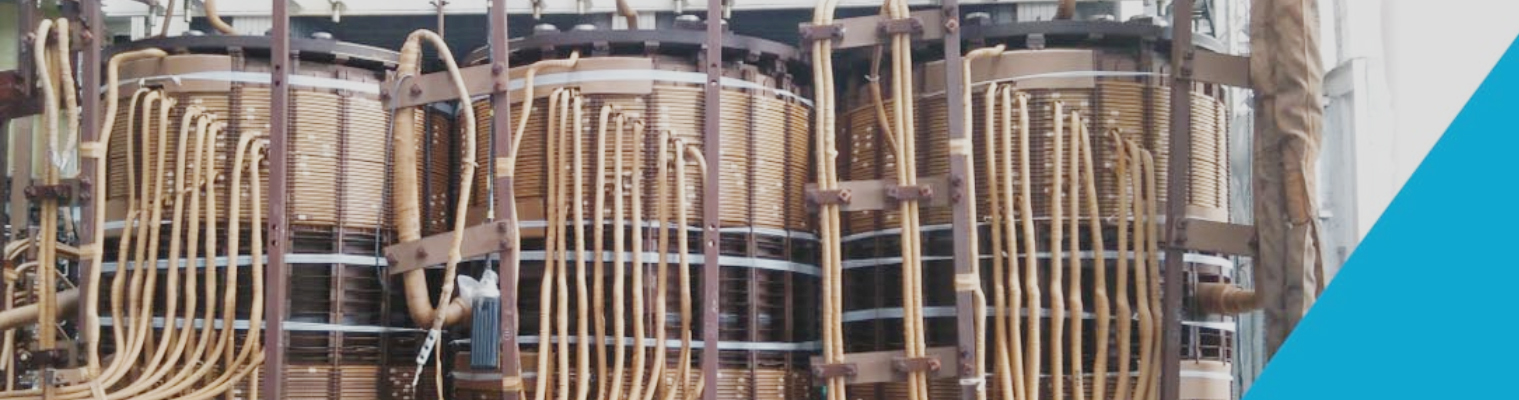
We have separate winding shop with 8 No. of Winding Machine Facility up to Manufacturing of 10 MVA 33 kV and Repair upto 50MVA 132kV Class Windings with only collapsible former & Electric Bending Machine & Hydraulic Shearing Machine in shop.

Disc winding is used for high voltage winding. For higher voltages the interleaved form of the disc winding has a great advantage to increase series capacitances and consequently to read more

DEHYDRATION

We have Dehydration Facility upto 100 MVA 220 kV Class
Another main component besides the core and the winding is the tank of a Power Transformer. It accommodates the active part and the oil filling. After vacuum drying process the active part is removed from the Oven and all components subject to the shrinkage are tightened again. The core & cel assembly is then placed into the tank and property lacked up during the transformer manufacturing process.

The temperature and exposure time is monitored during this time to ensure that the transformer is not too cool by the time it is get off from the oven. While in higher rating transformer, the vacuum is drawn for a period of time dependent on the voltage of the unit and time for which the active part was exposed to the atmosphere and the humidity at the time. The vacuum period is between 12 to 35 hours. Meanwhile the external wiring and termination work to be completed as per customer requirements.

Assemble

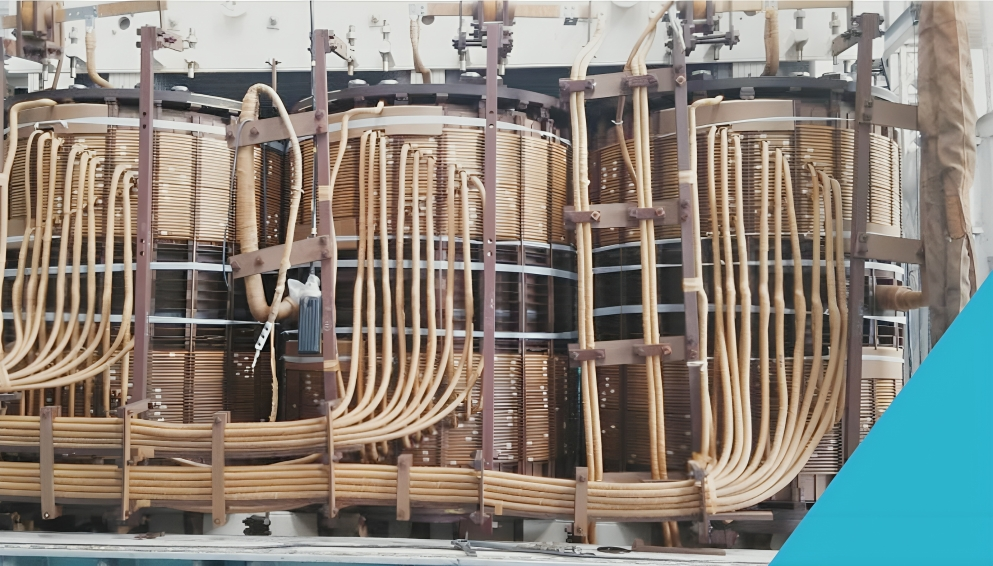
At the assembly stage, the mechanical stability of the windings plays a particularly important role.

End and tapping leads of all the windings are connected by special extra flexible, insulated copper cables, which are rigidly braced in position. In oil forced units, oil is circulated inside the winding by specially designed pipes of insulated materials.

High mechanical rigidity is achieved by hydraulic pressing at calculated force and tightening all pressure screws. The core-coil assembly is put into the oven for dehydration process.

OUR TESTING FACILITY

We have in house Heat Run Facility up to 10 MVA 33 kV Class at Our plant.

The process of manufacturing quality transformers is critically dependent on testing of raw materials, components and final assembled product. We are equipped with state of the art testing facilities to perform all routine and special tests.

The design element quality control is carried out at each manufacturing step. The final tests are made at the automated test field. Our transformers go through various below tests in our laboratory order to deliver the best of the transformers that are reliable and maintenance free.

FINAL TESTING

  • Heat Run Test
  • Electromagnetic tests
  • Excitation current of transformer
  • Dielectric tests
  • Load loss and No load losses
  • Insulating strength measurements
  • Noise-level measurements
  • Temperature rise test
  • Tan Delta Test
  • BDV Test